CAS530-62-1 Factory: Quality Production Solutions

All Categories

cas530-62-1 factory

A cas530-62-1 factory specializes in the production and manufacturing of phenanthrene, a polycyclic aromatic hydrocarbon compound identified by the CAS number 530-62-1. This chemical compound serves as a critical raw material in various industrial applications, making the cas530-62-1 factory an essential component of the global chemical supply chain. The primary function of such facilities involves synthesizing, purifying, and packaging phenanthrene to meet stringent quality standards required by diverse industries. These manufacturing plants employ advanced chemical processing technologies to ensure consistent product quality and high purity levels. The technological infrastructure within a cas530-62-1 factory typically includes distillation units, crystallization systems, and sophisticated quality control laboratories equipped with analytical instruments such as gas chromatography and mass spectrometry. These facilities maintain strict environmental controls and safety protocols to handle the chemical processes involved in phenanthrene production. Applications of the compound manufactured at a cas530-62-1 factory span multiple sectors, including pharmaceuticals, dyes and pigments, agricultural chemicals, and polymer manufacturing. The compound serves as an intermediate in synthesizing various pharmaceutical compounds and plays a vital role in producing specialty chemicals. Modern cas530-62-1 factory operations integrate automation systems and real-time monitoring technologies to optimize production efficiency and maintain product consistency. These facilities must comply with international chemical safety standards and environmental regulations, ensuring responsible manufacturing practices while meeting the growing market demand for high-quality phenanthrene products across industrial sectors worldwide.

Popular Products

Choosing a reliable cas530-62-1 factory offers significant practical benefits that directly impact your business operations and bottom line. First, established manufacturing facilities provide consistent product quality with verified purity levels, ensuring your downstream processes run smoothly without unexpected chemical variations. This reliability eliminates costly production disruptions and reduces waste from substandard materials. The operational benefits extend to supply chain stability, as reputable factories maintain adequate inventory levels and established logistics networks, guaranteeing timely delivery that keeps your production schedules on track. When you partner with an experienced cas530-62-1 factory, you gain access to technical support teams who understand your application requirements and can provide guidance on optimal usage parameters. This expertise proves invaluable when troubleshooting process challenges or exploring new product development opportunities. Cost efficiency represents another compelling advantage, as large-scale manufacturing facilities achieve economies of scale that translate into competitive pricing without compromising quality standards. The application suitability factor cannot be overlooked, as professional cas530-62-1 factory operations offer customized specifications and packaging options tailored to your specific industry needs, whether pharmaceutical-grade purity or industrial-scale bulk quantities. Regulatory compliance represents a critical decision factor, and established factories maintain comprehensive documentation including certificates of analysis, safety data sheets, and regulatory certifications that simplify your procurement processes and ensure compliance with industry standards. Environmental responsibility increasingly influences purchasing decisions, and modern cas530-62-1 factory facilities implement sustainable manufacturing practices, waste reduction programs, and emission control systems that align with corporate sustainability goals. Finally, long-term partnership potential with a dependable factory provides pricing stability, priority allocation during supply shortages, and collaborative opportunities for developing specialized product variants that give your business competitive advantages in evolving markets.

Practical Tips

Why Are Organophosphine Based Catalysts Essential for Semiconductor Packaging?

12

Dec

Why Are Organophosphine Based Catalysts Essential for Semiconductor Packaging?

The semiconductor industry relies on precise chemical processes that demand exceptional purity and reliability. Among the various catalyst systems employed in semiconductor packaging applications, organophosphine based catalysts have emerged as indis...
View More
How Do Thermally Latent Catalysts Improve Epoxy Molding Compound Storage Stability?

12

Dec

How Do Thermally Latent Catalysts Improve Epoxy Molding Compound Storage Stability?

Epoxy molding compounds are essential materials in electronics manufacturing, but their storage stability presents significant challenges for manufacturers and suppliers. The key to overcoming these challenges lies in understanding how thermally late...
View More
How is CDI coupling reagent used in large-scale manufacturing

07

Jan

How is CDI coupling reagent used in large-scale manufacturing

The pharmaceutical and chemical manufacturing industries increasingly rely on efficient coupling reagents to facilitate complex synthesis reactions at scale. Among these powerful chemical tools, cdi coupling reagent stands out as a versatile and reli...
View More
How Do Thermally Latent Catalysts Affect Reaction Rate and Thermal Properties?

05

Mar

How Do Thermally Latent Catalysts Affect Reaction Rate and Thermal Properties?

Thermally latent catalysts represent a revolutionary approach to controlling chemical reactions through temperature-dependent activation mechanisms. These specialized compounds remain inactive at room temperature but undergo rapid activation when hea...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

cas530-62-1 factory

Advanced Production Technology and Quality Control

Advanced Production Technology and Quality Control

A modern cas530-62-1 factory distinguishes itself through state-of-the-art production technology that ensures exceptional product quality and manufacturing efficiency. These facilities utilize multi-stage purification processes including fractional distillation, recrystallization, and advanced filtration systems that achieve purity levels exceeding industry standards. The integration of automated process control systems enables precise monitoring of critical parameters such as temperature, pressure, and reaction conditions throughout the manufacturing cycle. Quality assurance laboratories within the factory employ sophisticated analytical equipment including high-performance liquid chromatography, nuclear magnetic resonance spectroscopy, and inductively coupled plasma mass spectrometry to verify product specifications. This comprehensive testing regime ensures every batch meets stringent quality criteria before shipment. The technological investment demonstrates the factory's commitment to delivering consistent, high-purity phenanthrene that performs reliably in demanding applications. Furthermore, continuous improvement initiatives and regular equipment upgrades keep the facility at the forefront of chemical manufacturing capabilities, providing customers with access to the highest quality cas530-62-1 products available in the global market while maintaining competitive production costs through operational excellence.
Regulatory Compliance and Safety Standards

Regulatory Compliance and Safety Standards

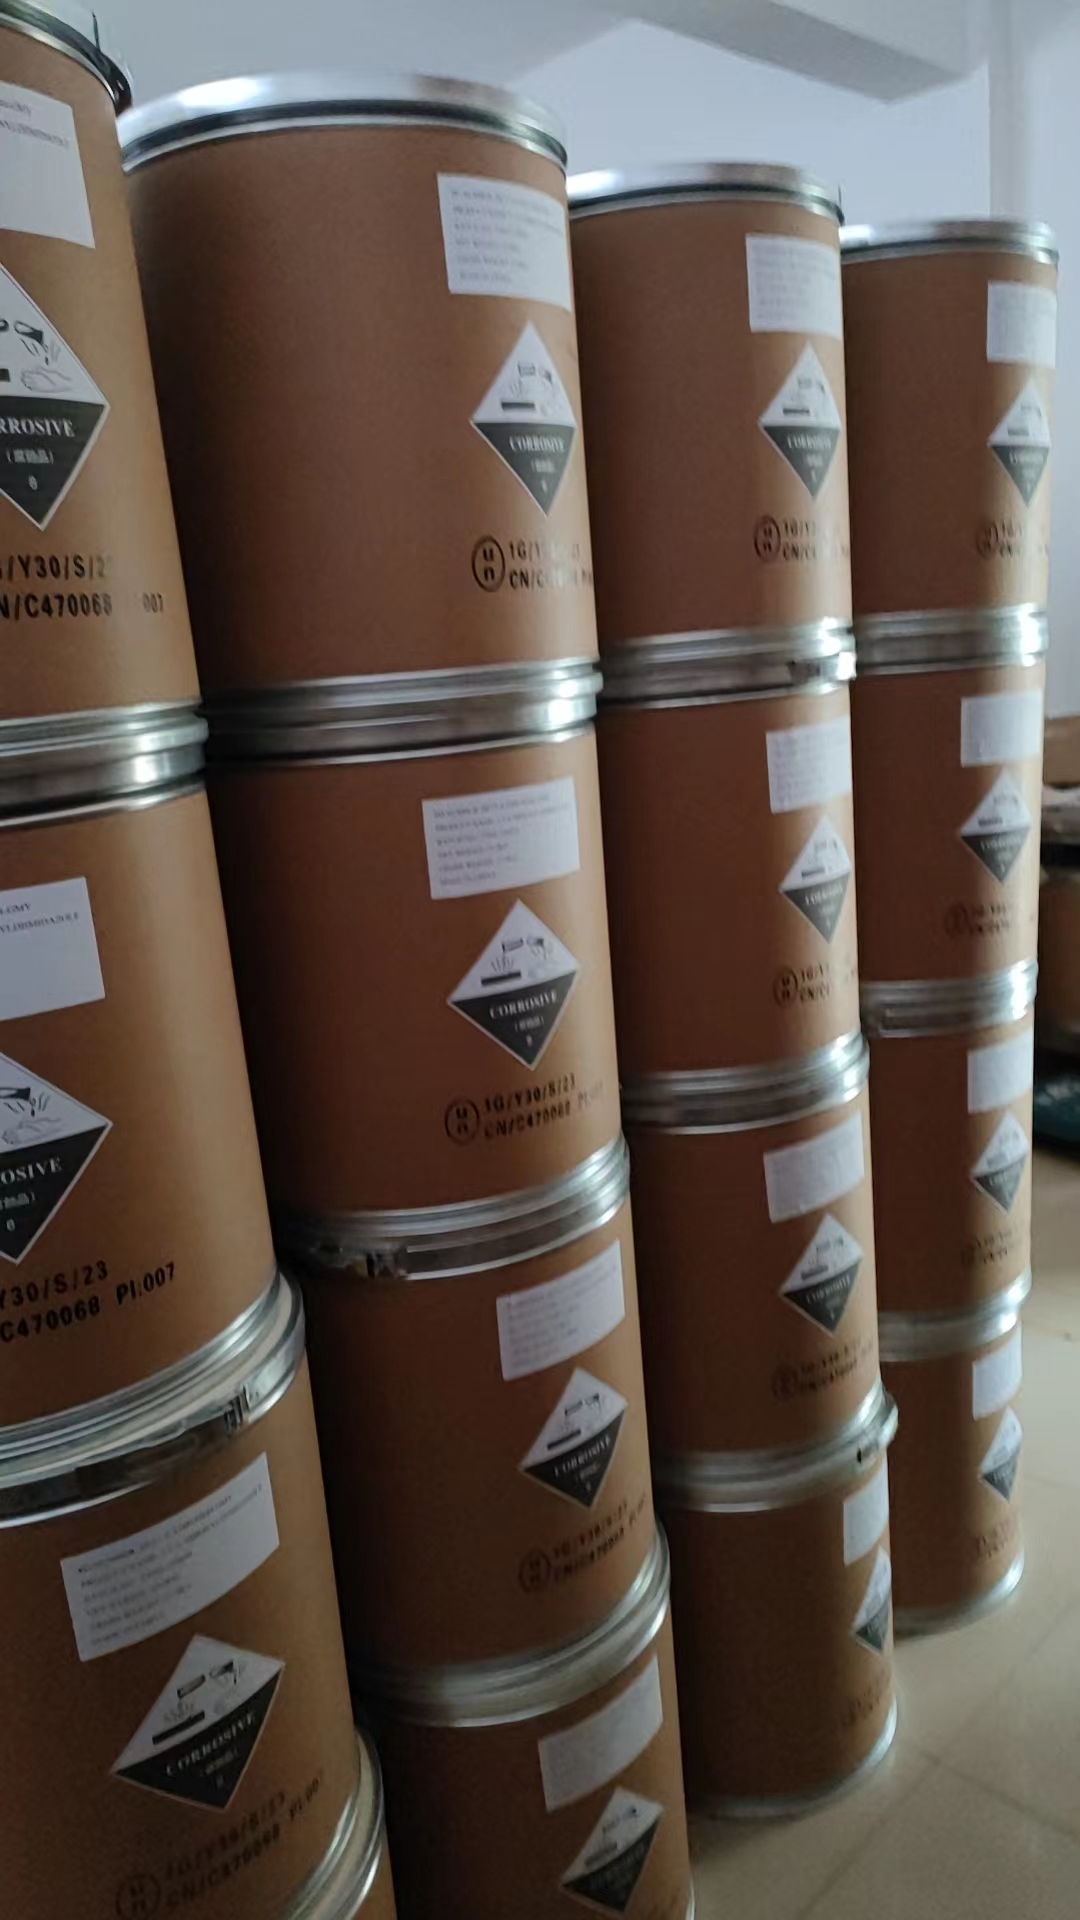
Operating a cas530-62-1 factory requires adherence to comprehensive regulatory frameworks and rigorous safety protocols that protect workers, communities, and the environment. Leading manufacturing facilities maintain certifications including ISO 9001 quality management systems, ISO 14001 environmental management standards, and OHSAS 18001 occupational health and safety certifications. These credentials validate the factory's commitment to responsible manufacturing practices and provide customers with confidence in product integrity and supply chain reliability. The facility implements robust safety management systems including hazard identification protocols, emergency response procedures, and regular safety training programs for all personnel handling chemical processes. Environmental stewardship represents a core operational principle, with factories investing in emission control technologies, wastewater treatment systems, and waste minimization strategies that minimize ecological impact. Regulatory documentation including detailed safety data sheets, material composition certificates, and traceability records accompany every shipment, simplifying customer compliance obligations and facilitating smooth customs clearance for international deliveries. This comprehensive approach to compliance and safety not only fulfills legal requirements but also demonstrates the cas530-62-1 factory's dedication to ethical business practices and sustainable operations that benefit all stakeholders throughout the value chain.
Flexible Supply Solutions and Customer Support

Flexible Supply Solutions and Customer Support

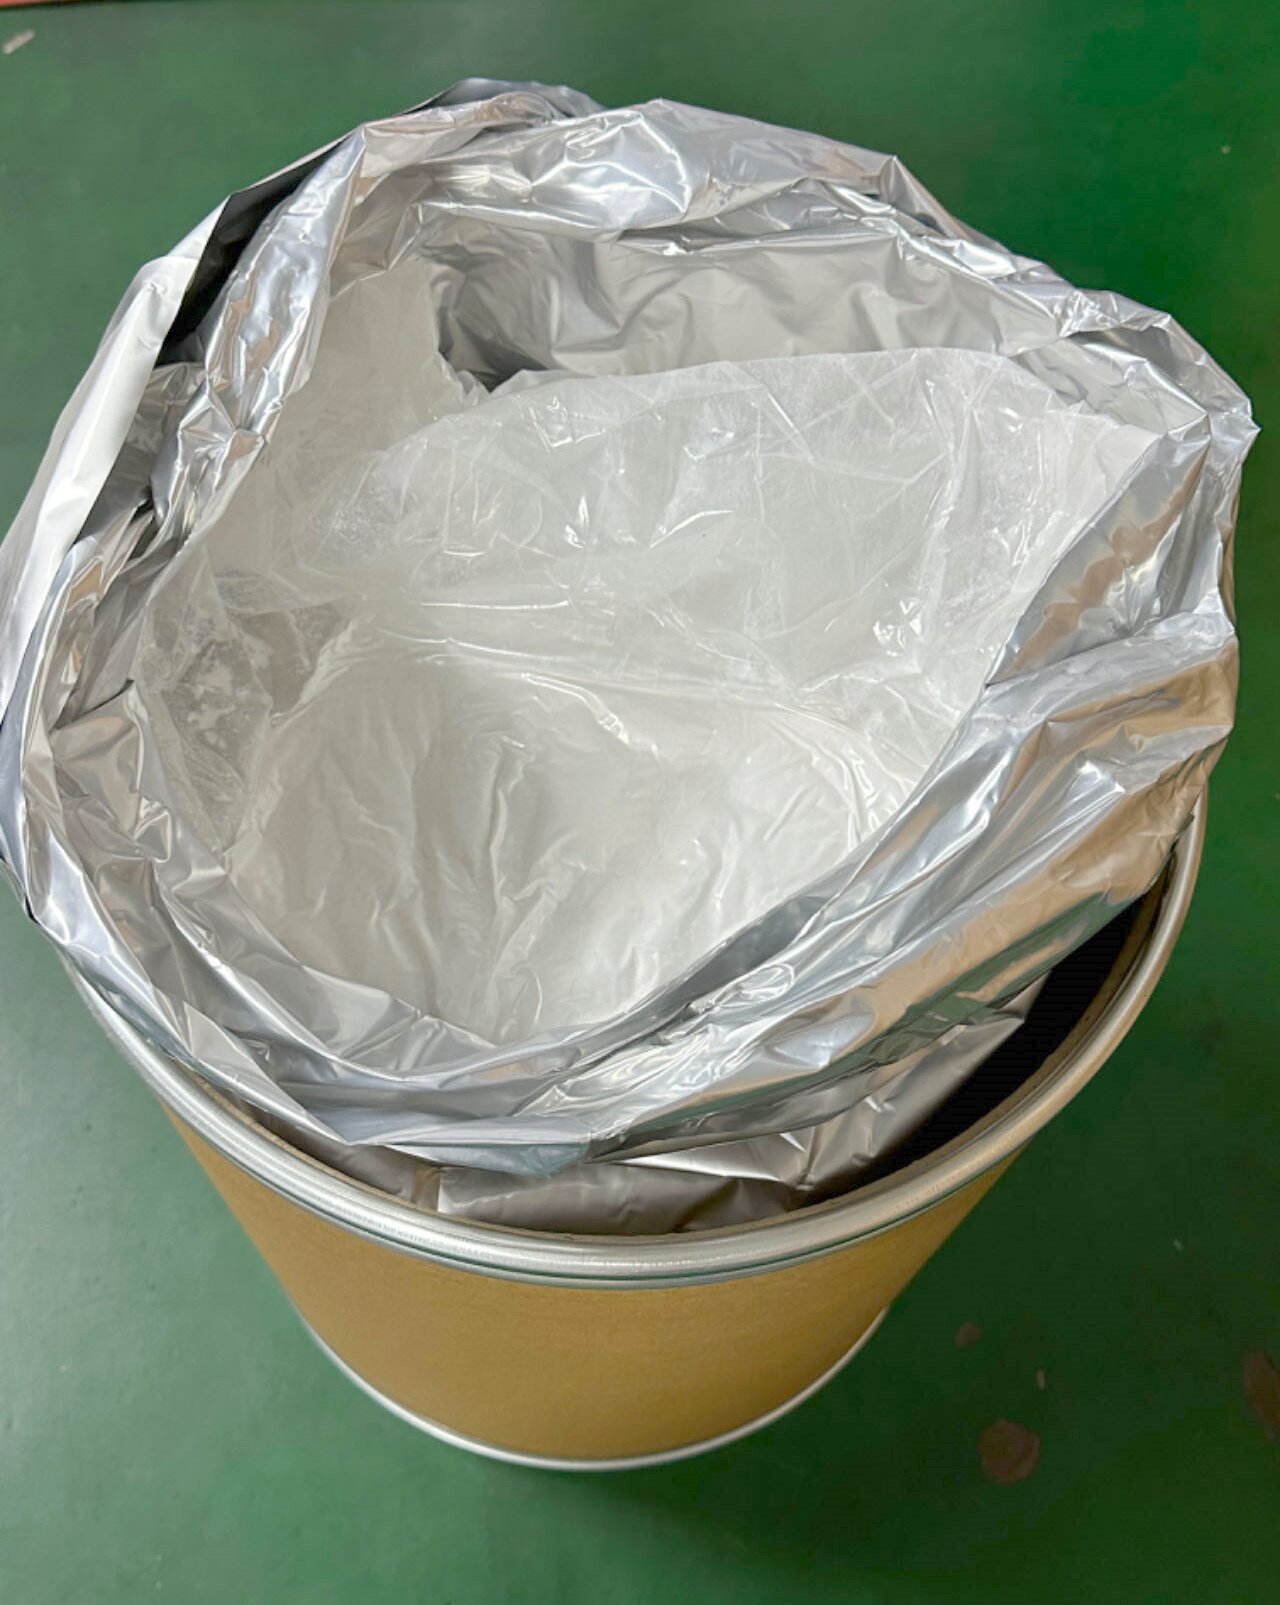
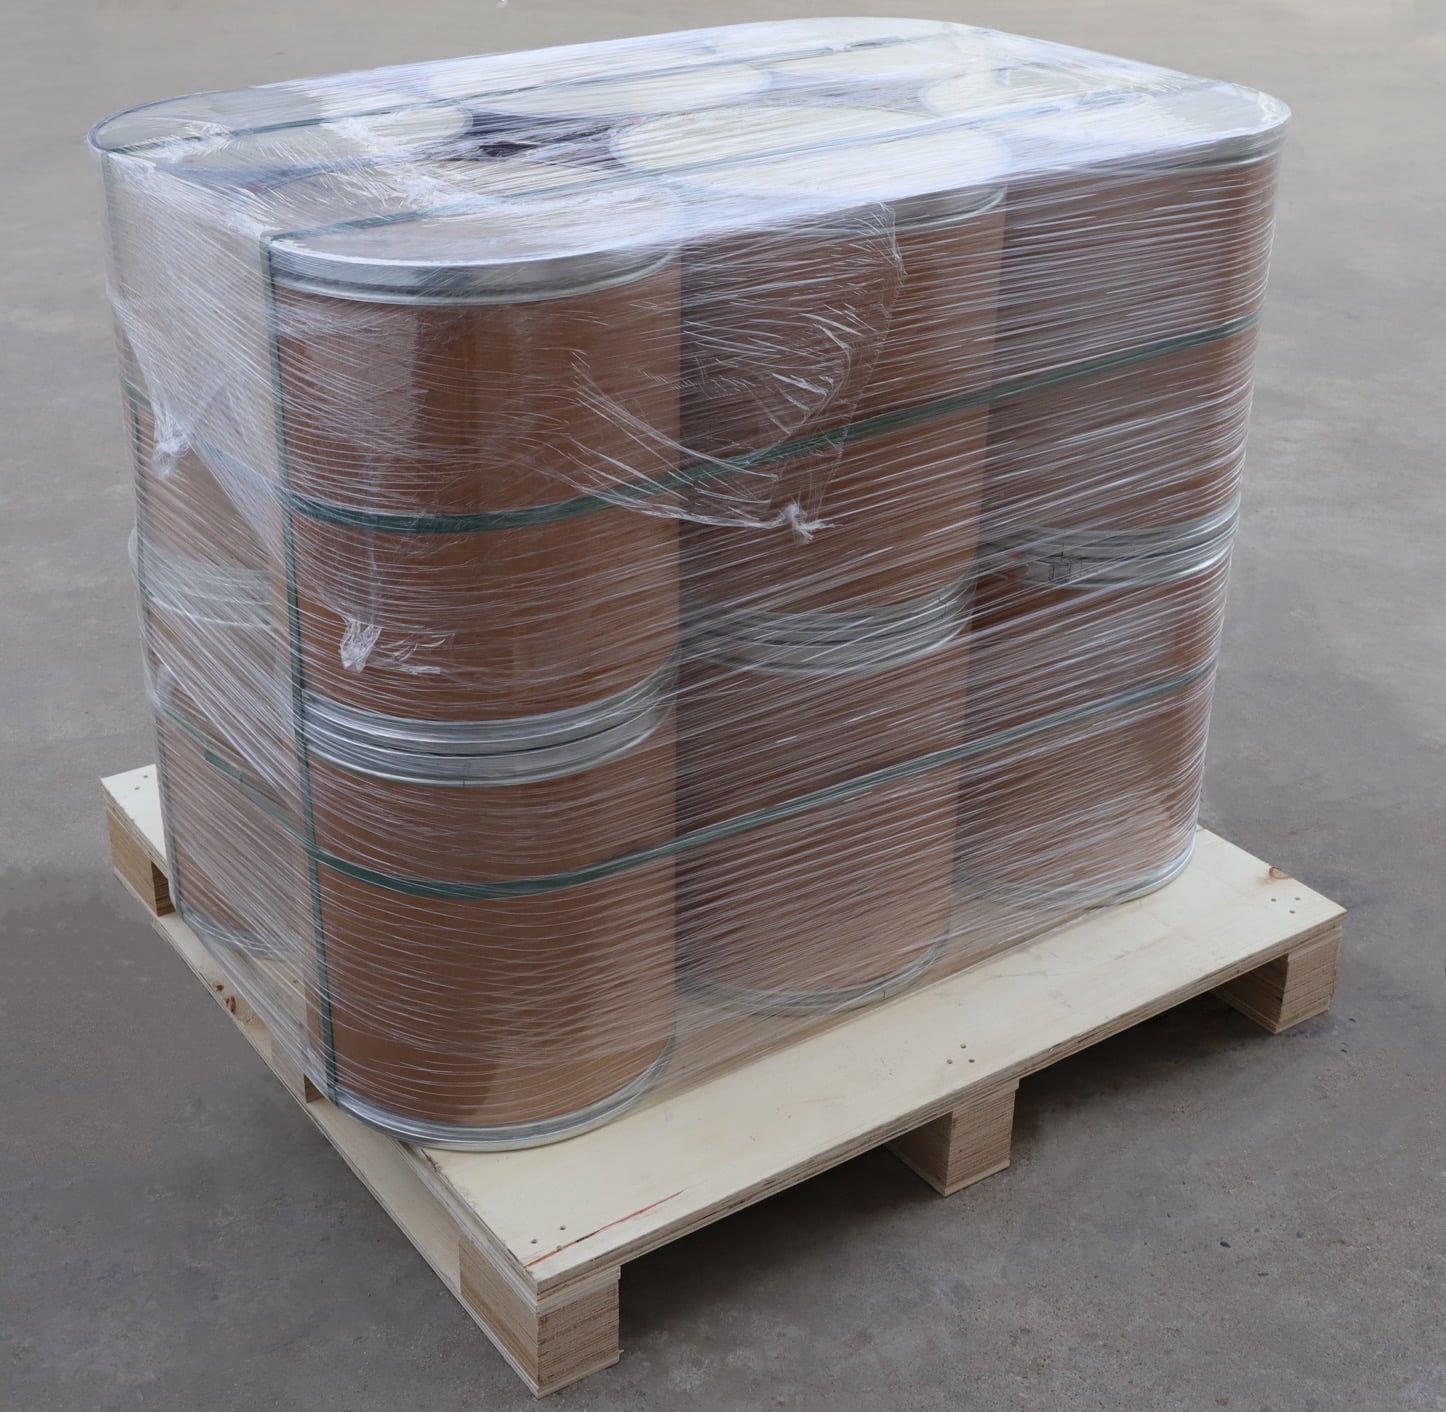
An exceptional cas530-62-1 factory differentiates itself through flexible supply arrangements and dedicated customer support services that address diverse business needs. These facilities offer scalable production capabilities that accommodate orders ranging from research-grade sample quantities to industrial-scale bulk shipments, providing solutions for companies at every stage of growth. Customization options include various packaging formats such as drums, totes, and specialized containers designed for specific handling requirements or storage conditions. The factory maintains strategic inventory reserves and implements demand forecasting systems that ensure product availability even during peak demand periods or supply chain disruptions. Experienced technical support teams provide valuable assistance with application optimization, product selection, and troubleshooting guidance, serving as an extension of your internal resources. Logistics coordination services streamline the ordering process with flexible shipping options, documentation support, and shipment tracking capabilities that provide visibility throughout the delivery cycle. Long-term partnership opportunities include volume pricing agreements, dedicated account management, and collaborative development programs for specialized product grades tailored to unique application requirements. This customer-centric approach transforms the cas530-62-1 factory from a simple supplier into a strategic partner invested in your success and committed to supporting your business objectives through reliable products and responsive service.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000